Veolia Electrodeionization EDI Stack Modules
Veolia E-Cell MK-5 EDI Stack with Up to 97% Recovery
1.Product OverviewThe Veolia E-Cell EDI MK-5 is an industrial electrodeionization (EDI) stack that uses electrical current to produce ultrapure water from suitably treated feed water. It is designed for continuous operation in semiconductor fabrication, power generation, solar panel prod
1. Product Overview
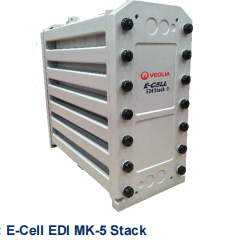
The Veolia E-Cell EDI MK-5 is an industrial electrodeionization (EDI) stack that uses electrical current to produce ultrapure water from suitably treated feed water. It is designed for continuous operation in semiconductor fabrication, power generation, solar panel production, green hydrogen generation and other heavy industrial applications.
2. PRODUCT SPECIFICATIONS
Item | Specification |
Brand | Veolia E-Cell |
Model | EDI MK-5 |
Product type | Industrial electrodeionization (EDI) stack |
Dimensions (W × H × D) | 30 × 61 × 72 cm (12 × 24 × 29 in.) |
Shipping weight | 165 kg (364 lb) |
3. OPERATING PARAMETERS
Parameter | Value / Range |
Nominal flow | 5.0 m³/h (22 gpm) |
Flow rate range | 2.3–6.4 m³/h (10–28 gpm) |
Recovery | Up to 97%; actual performance depends on site and design conditions |
Voltage | 0–400 VDC |
Amperage | 0–5.2 ADC |
Maximum inlet pressure | ≤ 6.9 bar (100 psi); actual inlet pressure depends on downstream product and concentrate pressure requirements, flow configuration and stack pressure drop |
Pressure drop | 1.4–2.8 bar (20–40 psi), at nominal flow and 25°C; verify for specific design conditions using the Winflows Design Simulator |
Feed water temperature | 4.4–40°C (40–104°F) |
Feed water pH | 4–11 |
Total exchangeable anions (TEA, as CaCO₃) | ≤ 65 ppm; table value applies at minimum flow and maximum temperature. The Winflows Design Simulator must be used to confirm acceptability for specific operating conditions |
Conductivity equivalent | ≤ 112 μS/cm |
Total hardness (as CaCO₃) | ≤ 1.0 ppm for standard counter-current operation; allowable hardness decreases to 0.1 ppm for co-current operation |
Silica (SiO₂) | ≤ 1.0 ppm; the allowable limit decreases above nominal flow and to 0.5 ppm when feed water hardness exceeds 0.5 ppm as CaCO₃ |
Total organic carbon (TOC, as C) | ≤ 0.5 ppm |
Total chlorine | ≤ 0.05 ppm |
Fe, Mn and H₂S | ≤ 0.01 ppm |
Boron | ≤ 1.0 ppm; limited to 0.3 ppm as B when a silica guarantee or a resistivity guarantee above 10 MOhm-cm is required |
Oil and grease | None detectable |
Oxidizing agents | None detectable |
Color | ≤ 5 APHA |
Particulate control | RO permeate or equivalent feed water. Systems with an open section between the RO system or other feed source and the EDI stack require filtration immediately before the stack |
Resistivity | ≥ 16 MOhm-cm; guarantee available for specified design conditions |
Sodium | ≤ 3 ppb; guarantee available for specified design conditions |
Silica product water | As low as 5 ppb; guarantee available for specified design conditions |
Boron product water | As low as 0.08 ppb; boron guarantees require confirmation with Veolia |
Typical sodium removal | ≥ 99.9%; typical removal efficiency, not an unconditional guarantee |
Typical silica removal | Up to 99%; typical removal efficiency, not an unconditional guarantee |
Typical boron removal | Up to 96%; typical removal efficiency, not an unconditional guarantee |
Actual product water quality and removal performance may vary depending on site conditions. Use Veolia’s Winflows Design Simulator and the E-Cell EDI Stack Owner’s Manual to verify feed water requirements and expected performance for the specific design conditions.
The stack is designed for continuous operation. It does not require caustic or acid regeneration of the ion exchange resin within the stack, and it does not require brine injection or concentrate recirculation.
4. Key Features & Benefits
Continuous electrodeionization operation: Uses electrical current to produce ultrapure water continuously without caustic or acid regeneration of the ion exchange resin within the stack.
High flow capacity: Provides a nominal flow of 5.0 m³/h, with a specified operating range of 2.3–6.4 m³/h for system capacity evaluation.
Counter-current operation: Helps minimize cleaning requirements at higher feed water hardness levels. The applicable hardness limit depends on the selected flow configuration.
No brine injection or concentrate recirculation: Simplifies concentrate-side system requirements.
Verified design performance: The Winflows Design Simulator can be used to evaluate expected product water quality and available performance guarantees for the specific design conditions.
Quality and compliance markings: CE, RoHS, CSA and EAC marked; certified with UKCA. The stack is manufactured in an ISO 9001 and ISO 14001 facility and is Halal certified by IFANCA®.
5. Key Applications
Ultrapure water for rinsing semiconductor chips, solar panels and other microelectronics.
Demineralized boiler feed water for high-pressure boilers in power plants and other heavy industrial sites.
Ultrapure water for electrolyzer green hydrogen generation.
Send Your Water Treatment Requirement
Tell us the feedwater, required capacity, target water quality and project conditions. Your inquiry email will automatically include the page you are viewing so our team can understand the exact product, technology or reference that led to your request.
- Feedwater source / available analysis
- Design flow or required production capacity
- Target product-water quality or process duty
- Project country, operating conditions and delivery target